by allen | Sep 18, 2026 | tool steel
After nearly 20 years in the tool steel industry, we have seen countless customers deal with chipped punches, cracked dies, premature wear, and unstable tool life because the steel selected at the beginning did not match the actual working conditions. Cold stamping...
by allen | Sep 18, 2026 | tool steel
Introduction: For global steel stockholders and regional distributors, maintaining market reputation relies on absolute material integrity. When a local steel trader unknowingly imports substandard or mislabeled tool steel (such as Cr12Mov passed off as genuine...
by allen | Sep 15, 2026 | tool steel
Introduction: A lower tool steel quotation may come from available stock or lower processing costs. But if the price is far below the market level, buyers should confirm whether the grade, melting route and inspection requirements are actually the same. This article...
by allen | Sep 15, 2026 | tool steel
A steel block arrives without visible defects. Its hardness meets the specification, and ultrasonic testing may show no rejectable indications. Several weeks or months later, the customer makes the first saw cut and finds internal cracks or white, flake-like defects....
by allen | Aug 28, 2026 | cold work tool steel
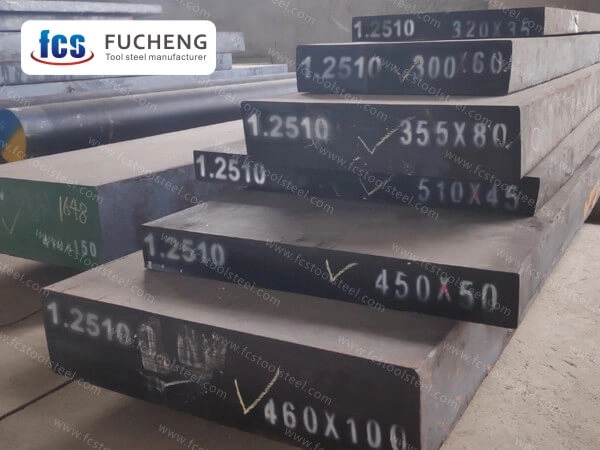
Pick the wrong tool steel, and you’ll find out the hard way—usually mid-run, when your blanking die starts chipping or your forming punch won’t hold an edge past a few thousand cycles. That’s the trap with 1.2510 and 1.2842: both are oil-hardening...
by allen | Aug 26, 2026 | tool steel
A cracked die insert mid-production run costs you more than scrap metal. It costs you downtime, deadlines, and the client’s patience. If you’ve ever watched a stamping tool fail prematurely and wondered whether you picked the wrong steel grade, you’re not alone....